
How weighing accuracy affects concrete batching systems

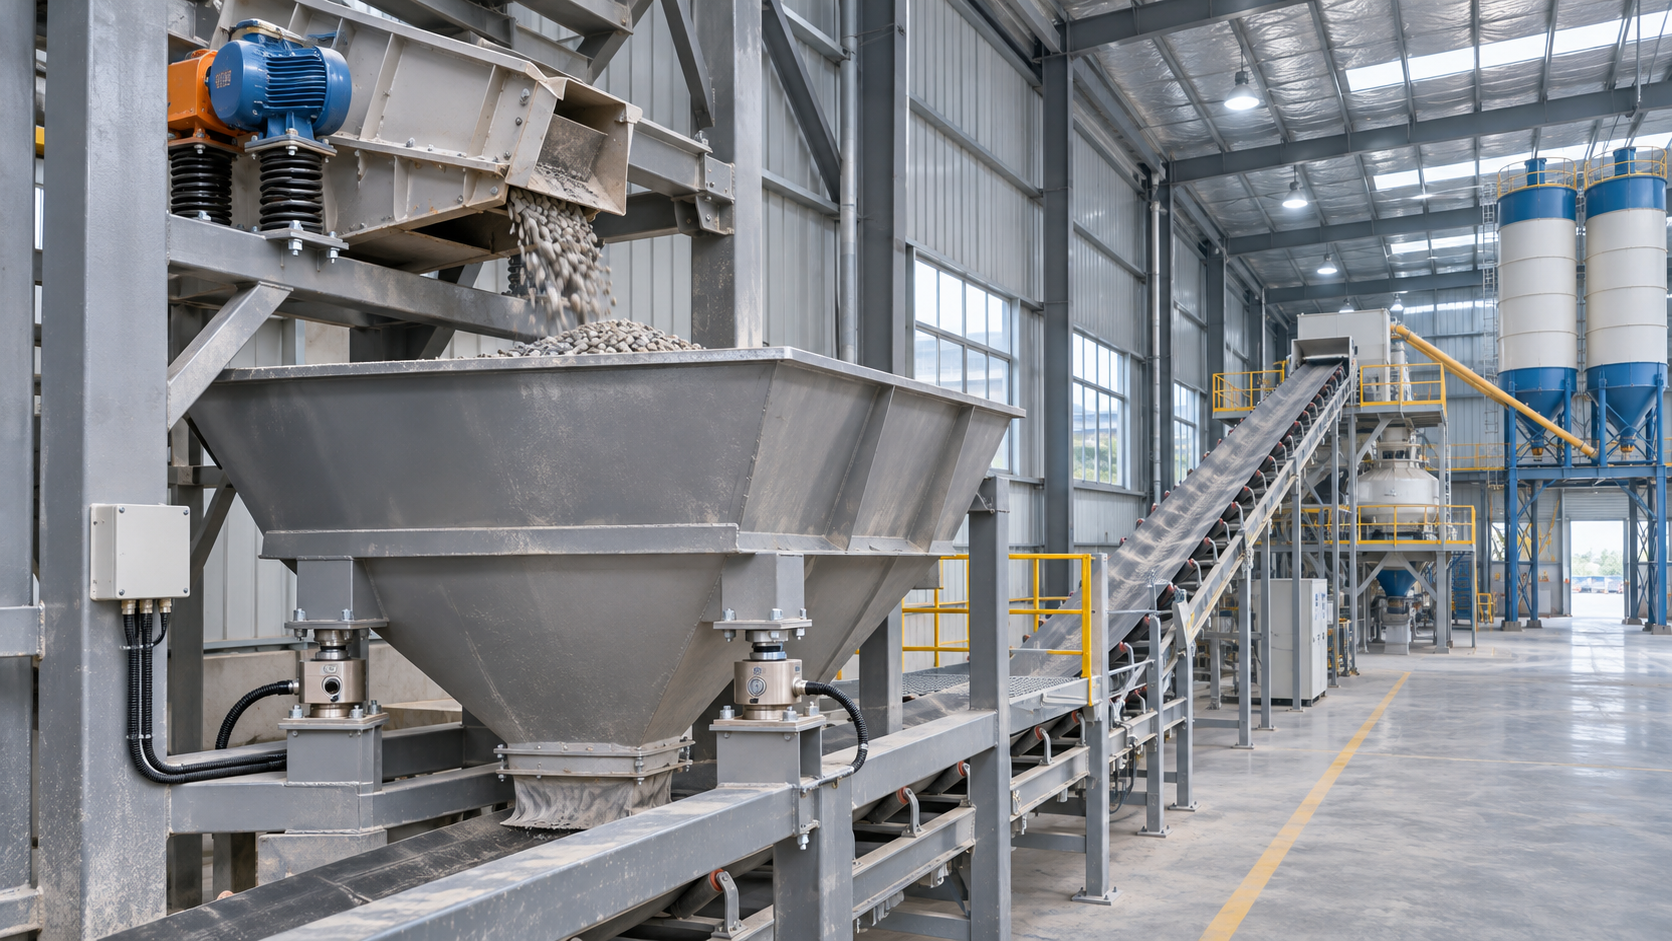
In concrete batching systems, weighing accuracy is more than a number on a controller screen. It influences the consistency of each mix, the amount of material consumed and the credibility of the production record. A small dosing error may seem harmless in isolation, yet repeated errors in water, cementitious materials or aggregate can change workability and make strength results harder to interpret.
For technical evaluators, the challenge is to look beyond a stated load-cell accuracy or a calibration certificate. A batching plant is a measurement chain: material enters a hopper, a weighing assembly responds, the controller decides when to stop the flow, and the actual batch is discharged. Every part of that chain can introduce error. Understanding where those errors arise makes it easier to compare plant capabilities under real production conditions.
Why weighing accuracy matters to the finished concrete
Concrete proportions are designed to work together. Cementitious materials, water, aggregates and admixtures each have a role, and an error in one constituent can affect the behavior of the whole batch. The most familiar example is the water-to-cementitious materials ratio, commonly written as w/cm. Too much effective water can increase workability while reducing the strength and durability potential expected from the mix. Too little can make the concrete difficult to place or compact.
Consider a simplified mix containing 300 kg of cementitious material and 150 kg of effective water. Its w/cm is 0.50. If the effective water rises by 6 kg while the cementitious mass remains unchanged, the ratio becomes 0.52. That difference does not, by itself, predict the concrete’s strength: curing, air content, materials and testing also matter. It does show why an apparently modest water error deserves attention, particularly when a mix is designed close to a specified limit.
Aggregate errors have a different character. An incorrect balance between sand and coarse aggregate can alter cohesion, finishability and pumping behavior. Inconsistent cement or supplementary cementitious material dosing can change paste volume and, depending on the material, influence setting and early-age strength. Admixtures are often dosed in much smaller quantities, so the same absolute error can represent a much larger percentage of the target.
Read the accuracy claim before comparing the plants
A supplier may describe a system as accurate to a percentage, but that figure is not useful until its reference is clear. Is the percentage based on the batch target, the scale’s full capacity, the displayed reading or a laboratory specification for the load cell? These are not interchangeable.
For example, an allowable error expressed as a percentage of a 2,000 kg scale capacity produces the same absolute error limit whether the target is 1,800 kg or 200 kg. At the smaller target, that absolute error represents a much larger share of the dose. A scale that performs acceptably on a full batch may therefore be a poor choice for frequent small batches or low-dose constituents.
When reviewing concrete batching systems, evaluators should ask for the following details together rather than treating any single number as conclusive:
- Weighing range and minimum practical load: the expected smallest and largest doses for each scale, including partial batches.
- Error basis: whether performance is stated as a percentage of target, indicated load or full scale, and whether it includes a fixed tolerance.
- Resolution and readability: the smallest displayed increment and how it relates to the dose being measured. Fine display increments alone do not prove accuracy.
- Operating conditions: vibration, temperature, material flow and other conditions under which the performance claim applies.
- Verification method: whether results come from static scale tests, dynamic batching tests or both.
Also distinguish accuracy from repeatability. A system can deliver nearly the same wrong amount in every batch, making it repeatable but biased. Conversely, an average close to the target can conceal substantial batch-to-batch variation. Both bias and spread matter when assessing production reliability.
From load cell to discharge: where errors enter
The weighing assembly
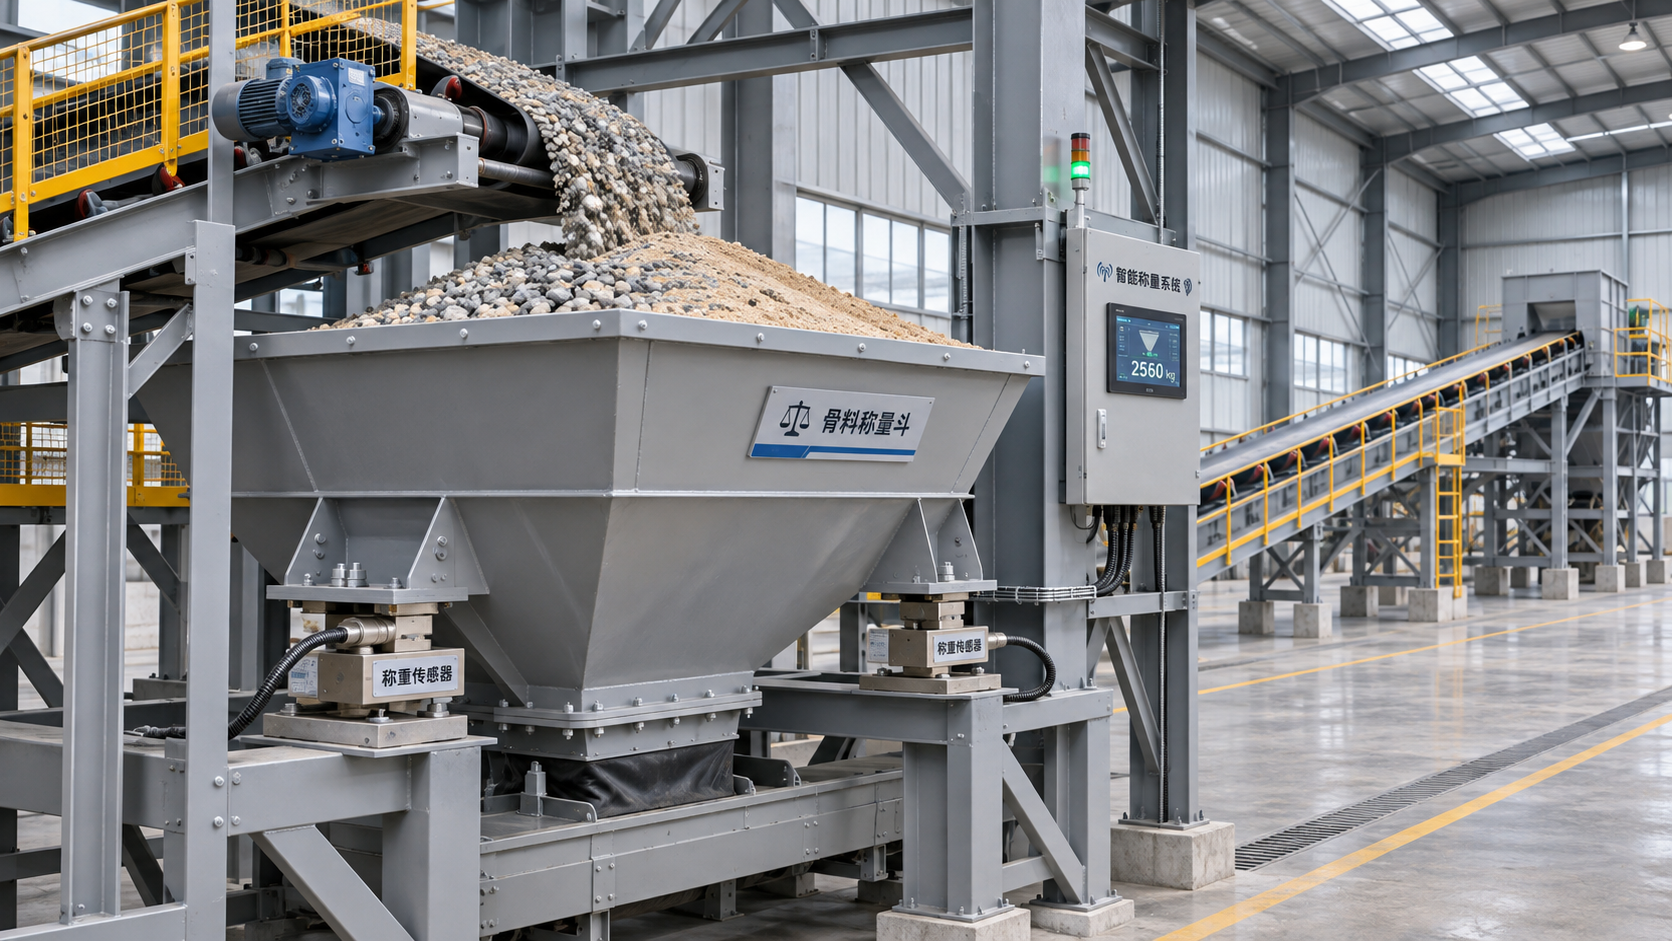
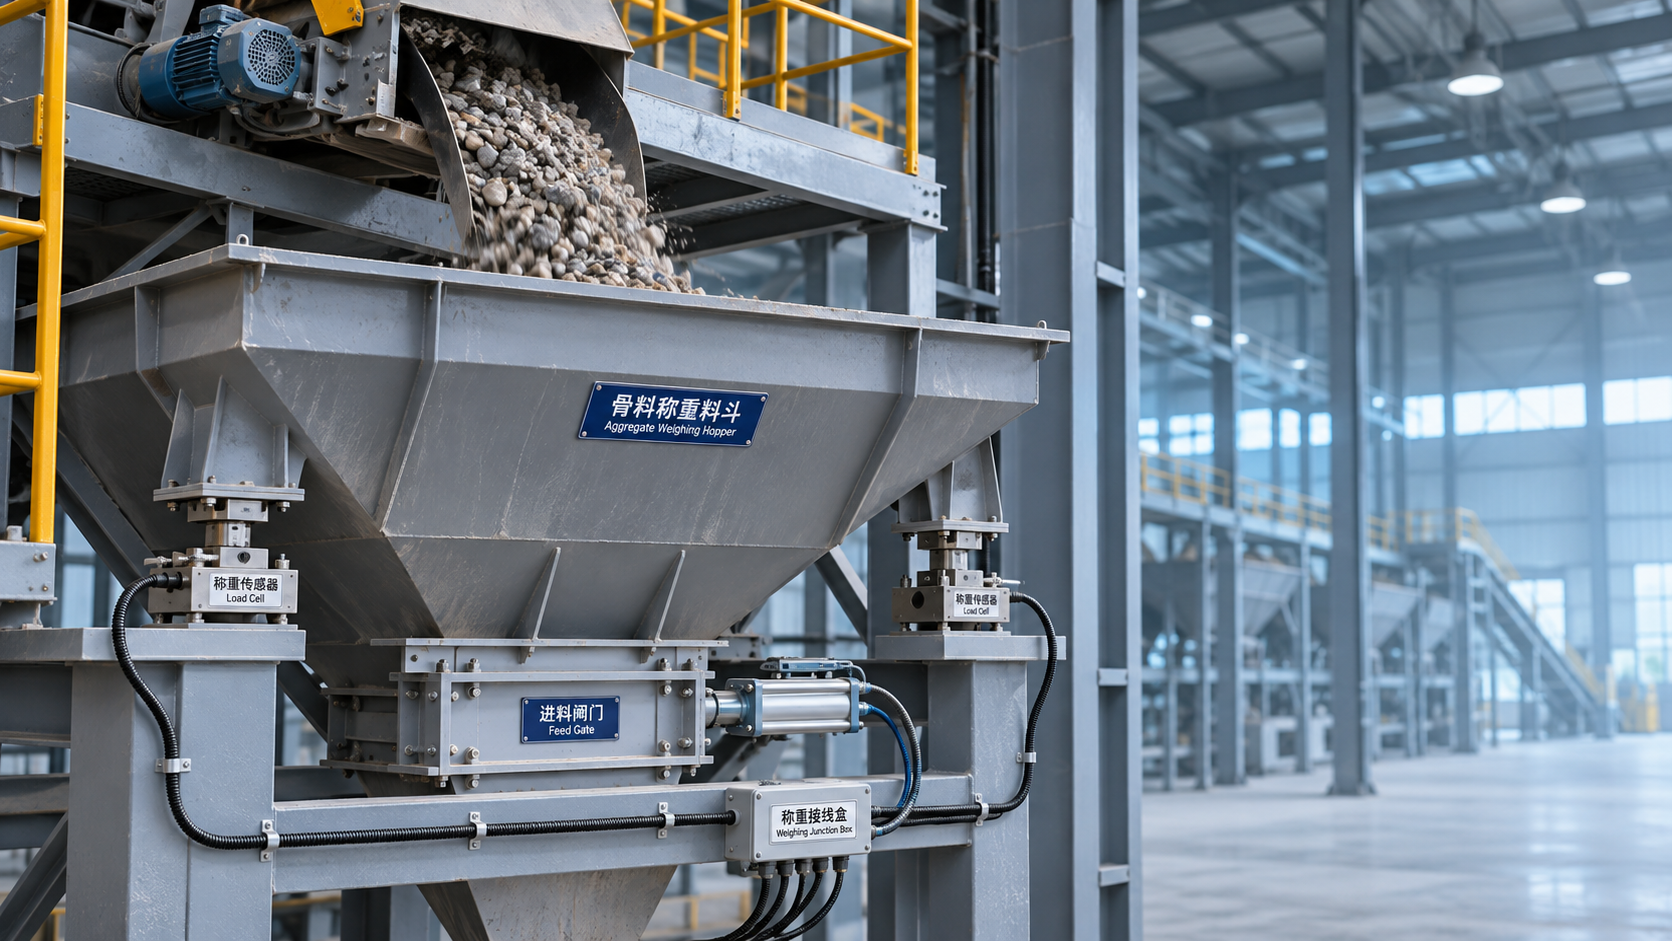
Load cells convert force into an electrical signal, but their rated performance is only one part of the installed system. Hopper supports, mounting hardware, cabling, signal conditioning and the controller all influence the result. A hopper that touches a frame, a stiff pipe or a buildup of hardened concrete may transfer part of the load outside the intended measurement path. The display can still look stable while the indicated weight is wrong.
Mechanical freedom is therefore as important as the sensor specification. Flexible connections must accommodate hopper movement without imposing significant force; supports should be installed and maintained as intended. Dirt, corrosion, damaged cables and water ingress also deserve attention during inspection. A plant with accessible scales and protected components is easier to keep accurate over its service life.
Material flow and controller response
Static calibration checks how a scale responds to known loads. It does not fully reproduce the movement of material during batching. Once a gate closes or a screw feeder stops, some material may still be in flight or continuing to discharge. The controller may use a preact, or cutoff correction, to stop feeding before the indicated weight reaches the target. If the correction is poorly tuned, the final dose can consistently overshoot or undershoot.
Flow behavior changes with material condition. Damp sand may move differently from dry sand; powder flow can vary with aeration or buildup. Vibration from nearby equipment can also make the signal fluctuate, prompting the controller to filter the reading. Excessive filtering may stabilize the display but delay the response used to stop the feeder. The right setting is a balance between signal stability and timely control.
Dynamic verification should therefore include repeated batches at representative production rates and target sizes. Record the final settled weight, the target and the deviation for each dose. A single successful batch tells an evaluator much less than a series that reveals drift, overshoot and variability.
Sequential weighing and cumulative error
Some plants weigh several ingredients sequentially in one hopper. This arrangement can be practical, but each addition depends on the previous reading and on the controller correctly identifying the incremental dose. Check how the system tares or calculates each increment, how it handles material already in flight and what happens when an ingredient exceeds its tolerance. The final total can appear reasonable even when individual ingredients are not proportioned as intended.
Moisture compensation: an accurate scale can still produce the wrong mix
Aggregates arrive with variable moisture. A scale measures the mass of wet aggregate, not dry aggregate alone, so part of the weighed material may be water. If that water is not accounted for, the batch can receive more effective mixing water than the design calls for, even when the water scale and aggregate scale both read correctly.
Absorption matters as well. Mix designs often express aggregate quantities on a saturated surface-dry basis. Free moisture above that condition contributes water to the mix; aggregate below that condition can absorb some mixing water. The controller’s correction method must match the basis used in the mix design and the moisture values entered by the operator.
Moisture probes can make corrections more responsive, but their output needs to represent the material actually being batched. Probe location, material contact, calibration and buildup can affect readings. Manual sampling remains useful for checking whether sensor values are credible. During an evaluation, ask how often moisture is measured, how corrections are calculated and whether the batch record preserves both measured values and any manual overrides.
Calibration, verification and applicable standards
Calibration and routine verification should not be treated as identical activities. Calibration establishes the relationship between a weighing system’s indication and reference loads under defined conditions; verification checks whether the system meets the applicable requirements. Site procedures may also include adjustment when results fall outside limits. The responsible team should document what was done rather than using the terms interchangeably.
For static checks, reference weights should be suitable for the test and traceable through an appropriate calibration system. Test points should cover the working range, especially normal operating loads and the smallest doses that matter. Depending on the scale and applicable procedure, the assessment may also consider zero stability, repeatability and the effect of load placement. Follow equipment instructions and relevant local requirements for safe testing.
Specifications vary by market and project. EN 206 addresses concrete specification, performance, production and conformity in the European context, while ASTM C94/C94M covers ready-mixed concrete in jurisdictions and contracts that adopt it. Weighing equipment may also be subject to local legal-metrology rules or requirements based on OIML R 76 for non-automatic weighing instruments, where applicable. Evaluators should consult the current adopted edition and the project documents rather than assuming one universal batching tolerance applies everywhere.
A certificate is a starting point, not a substitute for production evidence. Review the calibration date, test points, results before and after adjustment where available, identification of the instrument and the conditions of the test. After repairs to a load cell, hopper support or control system, determine whether re-verification is needed before normal production resumes.
A practical acceptance test for technical evaluators
Before comparing proposals, define the mixes and batch sizes the plant is expected to produce. A system optimized for large standard batches may behave differently when asked to produce a small specialty mix. Agree on acceptance criteria, test methods and responsibilities with the supplier before commissioning, using the governing project requirements as the reference.
- Inspect the installation. Check hopper clearance, supports, flexible connections, cable protection and access for maintenance. Look for contact points that could restrain the scale.
- Review static test results. Confirm that known-load tests cover relevant ranges and that reference equipment and records are identifiable.
- Run representative dynamic batches. Include typical and small target doses, normal material flow and repeated cycles. Compare final settled quantities with targets using the agreed method.
- Test control behavior. Observe alarms, tolerance limits, cutoff correction, operator overrides and the response to an out-of-tolerance dose. A warning is useful only if the procedure for responding to it is clear.
- Check moisture handling and records. Verify the aggregate moisture inputs, correction logic and treatment of added water. Confirm that reported quantities can be traced to each batch.
Pay particular attention to what the record calls “actual.” Does it represent the settled scale reading, a value captured before discharge, or simply the controller’s calculated target? Can the system preserve corrections and interventions without overwriting them? For a technical evaluator, trustworthy data is part of the equipment’s performance, not merely an administrative feature.
Accurate weighing will not eliminate every source of concrete variability. Materials still change, moisture measurements have limits, and mixing and delivery conditions matter. But a well-designed and verifiable weighing chain gives the production team a dependable starting point—and makes deviations easier to identify before they become repeated batches of uncertain concrete.
 How weighing accuracy affects concrete batching systemsTime : Nov 16, 2026
- How does a smart concrete batching plant improve weighing accuracy?Time : Nov 13, 2026
- How does digital batching plant control improve weighing accuracy?Time : Nov 03, 2026

Industry Briefing
Get the top 5 industry headlines delivered to your inbox every morning.